
 Business License
How Stainless Steel Wire Mesh Filters Are Manufactured: From Wire Drawing to Industrial Application
A stainless steel wire mesh filter is not simply “woven cloth cut to size.” The gap between a commodity mesh disc and a precision-engineered filter element comes down to manufacturing control — wire tolerance, annealing, weave stability, welding, cleaning, and inspection. This article walks through the production process and maps each stage to the industries that depend on it.
The Manufacturing Chain
1. Wire Drawing & Annealing
Filter-grade stainless wire is drawn to tight diameter tolerances — typically ±0.001 mm for fine filtration grades. Controlled annealing relieves work-hardening and restores corrosion resistance. Wire diameter deviation is the single largest cause of micron-rating drift in finished mesh.
2. Precision Weaving
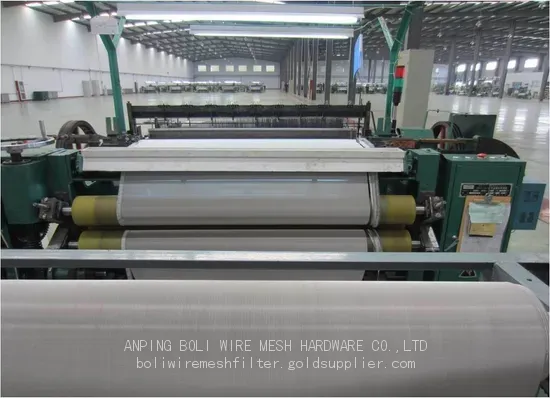
Warp and weft wires are interwoven on CNC looms under constant tension. For filter elements, twill weave and Dutch weave are preferred over plain weave because they lock wires more tightly and resist deformation under differential pressure. Reverse Dutch weave is specified when the mesh must survive high-pressure hydraulic service.
3. Cutting, Forming & Welding
Mesh is cut, rolled into cylinders, pleated, or formed into baskets. Welding is the critical step — and the reason 316L, not 316, is specified for welded elements. 316L’s 0.03% maximum carbon content prevents chromium carbide precipitation in the heat-affected zone, eliminating intergranular corrosion pathways.
4. Cleaning & Passivation
Elements undergo alkaline degreasing, acid pickling, and passivation (typically citric or nitric acid) to remove free iron, welding scale, and embedded contaminants. Pharmaceutical and food-contact filters require additional DI water rinsing and, in some cases, ultrasonic cleaning.
5. Inspection & Certification
Final QC includes bubble-point testing, micron rating verification, dimensional inspection, and pressure-drop measurement. Material certificates (EN 10204 3.1) and traceability documentation accompany every shipment.
Industry Mapping: Grade, Weave & Micron
| Industry | Typical Grade | Weave | Micron Range | Key Requirement |
|---|---|---|---|---|
| Pharmaceutical | 316L | Twill / Dutch | 5–50 µm | Cleanability, no leaching |
| Food & Beverage | 304 / 316L | Plain / Twill | 50–500 µm | Hygiene, CIP compatibility |
| Hydraulic & Fuel | 316L | Reverse Dutch | 3–25 µm | Pressure tolerance |
| Chemical Processing | 316 / 316L | Dutch / Twill | 10–200 µm | Chloride resistance |
| Water Treatment | 316 | Plain / Twill | 50–300 µm | Flow rate, backwash |
| Aerospace | 316L | Twill / Sintered | 2–40 µm | Absolute rating, reliability |
| Polymer & Melt | 316L | Reverse Dutch | 20–150 µm | High differential pressure |
Process-Driven Specification Notes
Pharmaceutical filtration: Element must be 316L, welded, passivated, and bubble-point tested. Sintered multilayer mesh is often preferred over single-layer weave for absolute ratings and repeated SIP/CIP cycles.
Hydraulic filtration: Reverse Dutch weave in 316L is the industry standard. The heavy warp wires resist collapse under 200+ bar differential pressure that would deform plain weave cloth.
Chemical processing: Chloride concentration drives grade selection. Below 200 ppm, 304 may suffice; above it, 316 or 316L is required. Molybdenum content (2–3%) provides the pitting resistance.
Food and beverage: 304 is acceptable for non-welded sieving screens. Welded filter assemblies, sterilisation cycles, and acidic product contact shift the specification to 316L.
Why Manufacturing Control Matters More Than Material Price
The material cost difference between 304 and 316L mesh is roughly 25–50%. But the cost of a failed filter element — unplanned downtime, product contamination, batch rejection, or regulatory non-compliance — typically exceeds that difference by orders of magnitude.
At BOLI Wire Mesh (www.boliwiremesh.com), every filter and strainer element is produced under controlled wire drawing, precision weaving, certified welding, and documented inspection. We supply 304, 316, and 316L elements in plain, twill, Dutch, and reverse Dutch weave, with micron ratings from 1 µm to 300 µm and full material traceability.
Send your medium, temperature, pressure, and micron requirement — our engineering team will return a specification and quotation within 24 hours.
Request a Quote →
FAQ
Why is 316L preferred over 316 for welded filter elements?
Because 316L’s low carbon content (≤0.03%) prevents sensitisation during welding, avoiding intergranular corrosion that standard 316 cannot resist after thermal exposure.
What weave is best for high-pressure hydraulic filters?
Reverse Dutch weave in 316L — it offers the highest mechanical strength and resists deformation under high differential pressure.
Do you provide bubble-point test data?
Yes. Bubble-point and micron-rating test reports are available on request for all precision filter elements.
Recently Posted
-
Sintered vs. Woven Stainless Steel Wire Mesh Filters: Which One Fits Your Process?
October 10, 2026Two filters can share the same 316L grade, the same 25 µm rating, and the same outer dimensions — yet behave completely differentl Read More
-
Stainless Steel Wire Mesh Weave Types: Plain, Twill & Dutch Weave Explained
October 10, 2026Stainless Steel Wire Mesh Weave Types: Plain, Twill & Dutch Weave ExplainedChoosing the right stainless steel wire mesh cloth Read More
-
304/316/316L Stainless Steel Wire Mesh Filters & Strainers: A Complete Selection Guide for Engineers
October 10, 2026Specifying a stainless steel wire mesh filter or strainer is not a “one-grade-fits-all” decision. A 304 mesh that performs flawles Read More
-
304 vs 316 vs 316L Stainless Steel Wire Mesh Cloth: Which Grade Should You Specify for Your Application?
October 10, 2026304 vs 316 vs 316L Stainless Steel Wire Mesh Cloth: Which Grade Should You Specify for Your Application?Choosing the wrong stainle Read More

Contact Us

Recommended Products
-
 Stainless Steel Perforated Strainer .oil Mesh Filter Air Filter Mesh StrainerUS$ 1 - 20MOQ: 10 Bags
-
AISI 304 316 316L Plain Weave Woven Stainless Steel Wire Netting For Oil Filter Air Filter MakingUS$ 1.0 - 10.0MOQ: 10 Square Feet
-
Factory Manufacturer Woven Stainless Steel Wire Mesh Screen on Sale Wholesale SUS 304 316 Stainless Steel Wire Mesh High Strength AISI304 Stainless Steel Filter Screen Reverse Dutch Wire Mesh 4 8 20 100 120 200 250 Mesh Stainless Steel Woven Filter MeshUS$ 1.0 - 10.0MOQ: 10 Square Feet
-
Qualified Plain Weave Woven Stainless Steel Wire Mesh Screen on Sale Wholesale SUS 304 316 Stainless Steel Wire Mesh High Strength AISI304 Stainless Steel Filter Screen Reverse Dutch Wire Mesh 4 8 20 100 120 200 250 Mesh Stainless Steel Woven Filter MeshUS$ 1.0 - 10.0MOQ: 10 Square Feet
-
100% Food Grade Nylon Mesh White Color Nylon Mesh Cloth Food Grade 8um 10um 200um 60um 100um 600um Nylon MeshUS$ 1 - 20MOQ: 10 Square Meters
-
Nylon Filter Cloth Food Grade 8um 10um 200um 60um 100um 600um Nylon MeshUS$ 1 - 20MOQ: 10 Square Meters
-
SS304 316 Stainless Steel Perforated Filter Cartridge With Flange and Handle Accept OEM.factory SupplierUS$ 1 - 20MOQ: 10 Bags
-
Stainless Steel Wire Mesh Filter Cartridges Filter Cylinder Bucket Strainer Mesh for Beer FiltrationUS$ 1 - 20MOQ: 10 Bags
-
Wholesale SUS 304 316 Stainless Steel Wire Mesh High Strength AISI304 Stainless Steel Filter Screen Reverse Dutch Wire Mesh Stainless Steel Wire Cloth Mesh 4 8 20 100 120 200 250 300 325 635 2000 3500 Mesh Stainless Steel Woven Filter MeshUS$ 1.0 - 10.0MOQ: 10 Square Feet
-
BOLI QUALITY Kitchen Accessories Sink Waste Filter Net Strainer Mesh Drain Strainer Drain Filter Strainer Basket Strainer BL021US$ 1 - 20MOQ: 10 Bags
-
Mesh Perforated Mesh Filter Bucket Strainer Basket/ Sintered Stainless Steel Wire Mesh Cone Filter/Perforated Wire Mesh Filter Bucket StrainerUS$ 1 - 20MOQ: 10 Bags
-
Nylon Filter Cloth 80-500 Mesh White Screen Filtration Food Grade Water Industrial ClothUS$ 1 - 20MOQ: 10 Square Meters
-
FDA Food Grade Nylon Filter Mesh/ 100 220 500 Micron Food Grade Nylon Filter Mesh ClothUS$ 1 - 20MOQ: 10 Square Meters
-
Polyester Steel Breaker Fabric Tear-Resistant Dipped Steel Cord Fabric Nylon Brass Coated Steel Cord for Making Tyre 2*0.30mm Belt/Tear-Resistant Dipped Steel Cord Fabric for Conveyor Belt Tear-Resistant Dipped Steel Cord Fabric for Conveyor BeltUS$ 1 - 200MOQ: 10 Kilometers
-
Tear-Resistant Dipped Steel Cord Fabric Nylon Brass Coated Steel Cord for Making Tyre 2*0.30mm Belt/Tear-Resistant Dipped Steel Cord Fabric for Conveyor Belt Tear-Resistant Dipped Steel Cord Fabric for Conveyor BeltUS$ 1 - 200MOQ: 10 Kilometers
-
BOLI Steel Cord Fabric for Conveyor Belt IW/TW/SW Belt Woven Steel Cable/STEEL Cord Fabric for Rubber Conveyor BeltsUS$ 1 - 200MOQ: 10 Kilometers
-
Top Quality Industrial Walkways Heavy Steel Bar Grating.Hot Dip Galvanized Bar Steel Grating .Top QualityUS$ 1 - 200MOQ: 10 Square Meters
-
BOLI -Stainles Steel Floor Steel Grating China GOLD Suppliers Dustproof Feature Upper and Lower Clip Steel Grating Used for Showcase GroundUS$ 1 - 200MOQ: 10 Square Meters
-
BBQ MESH Crimped Wire Mesh for Mining Crusher Screen Wholesale High Quality Stainless Steel Crimped Mesh Screen 304 316 316LUS$ 1 - 20MOQ: 10 Square Meters
-
Carbon Steel Strong Quality Crimped Wire Mesh for Mining Crusher Screen Wholesale High Quality Stainless Steel Crimped Mesh Screen 304 316 316LUS$ 1 - 20MOQ: 10 Square Meters